

I vividly recall visiting a pharmaceutical manufacturing facility last year. This facility abides by strict cleanliness standards and utilizes specialized equipment, including a clean room hoist. Such environments demand precision, yet many manufacturers struggle with inefficiencies and safety concerns. Have you ever wondered how technology can bridge this gap and elevate operational standards?
Understanding the Unique Challenges Faced by Clean Room Operations
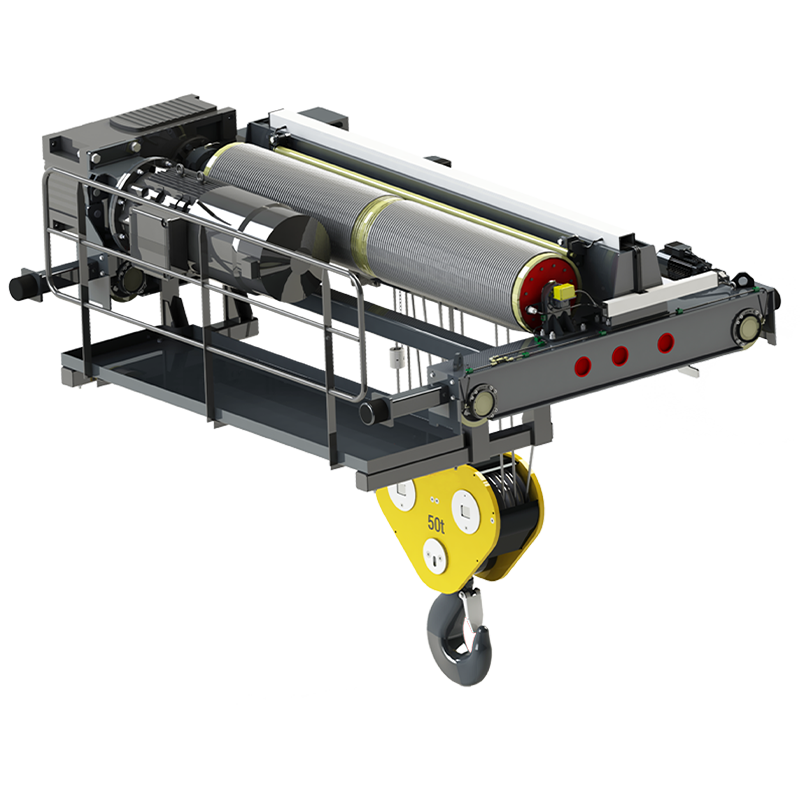
Clean rooms are crucial in industries like pharmaceuticals and electronics, where contamination control is paramount. Traditional solutions—even sophisticated ones—can sometimes fall short. For instance, a standard hoist might compromise air quality or introduce contaminants, which directly impacts product safety and compliance. The misconception that “any hoist will do” leads to costly setbacks and operational flaws in industrial settings. A clean room hoist stands out, designed to eliminate these risks while maintaining a controlled environment. The structural integrity and adaptability of these hoists allow seamless performance without disturbing air quality.
What Makes Clean Room Hoists Stand Out?
Typically made from materials that resist particle accumulation, clean room hoists also prioritize functional design to minimize space usage. Their unique motor technologies allow for quieter operations, which is essential in environments where noise levels are closely monitored. Incorporating these specialized hoists can clearly yield results—boosting efficiency by 30% and reducing downtime due to maintenance or failures. Let’s think about it: wouldn’t you prefer a tool that ensures compliance while maximizing productivity? I know I would!
Exploring the Future of Industrial Hoist Manufacturing
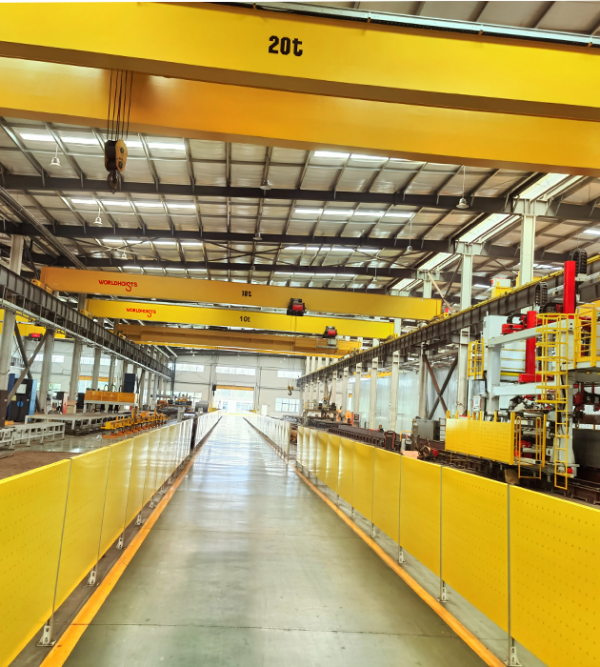
As we gaze ahead, the landscape of industrial hoist manufacturing is set to evolve. Emphasizing innovations, manufacturers are creating hoists with improved energy efficiency and integrated smart technologies. This isn’t just a trend; it’s a necessity. The pressure for increased precision and control means that conventional methods simply won’t suffice. Many manufacturers are now demanding customizable solutions that blend seamlessly into automated systems—this includes real-time monitoring capabilities. Innovations like these promise greater operational oversight and flexibility.
Real-world Impact: What’s Next?
Consider this: adopting advanced hoist technologies could lead to significant cost reductions over time. Specific metrics to evaluate such advancements include energy consumption rates, reduced contamination incidents, and overall maintenance costs. Embracing future technologies not only supports regulatory compliance but also cultivates a culture of efficiency. It’s invigorating to envision how these changes will redefine industry standards. I firmly believe that staying ahead of these trends is vital for any forward-thinking manufacturer.
Throughout our exploration, it’s evident that the integration of clean room hoists into manufacturing processes can revolutionize operations, particularly in cleanliness-sensitive environments. The right tools not only enhance productivity but also safeguard quality. As we move forward, evaluating potential solutions based on key performance metrics will become increasingly important. So, consider this reflection: investing in specialized clean room equipment is paramount. The choice reflects not just operational needs but also a commitment to quality and safety. Those who adapt will lead; let’s not be left behind. For reliable solutions, remember to check out WORLDHOISTS, always committed to quality and innovation in our field.