

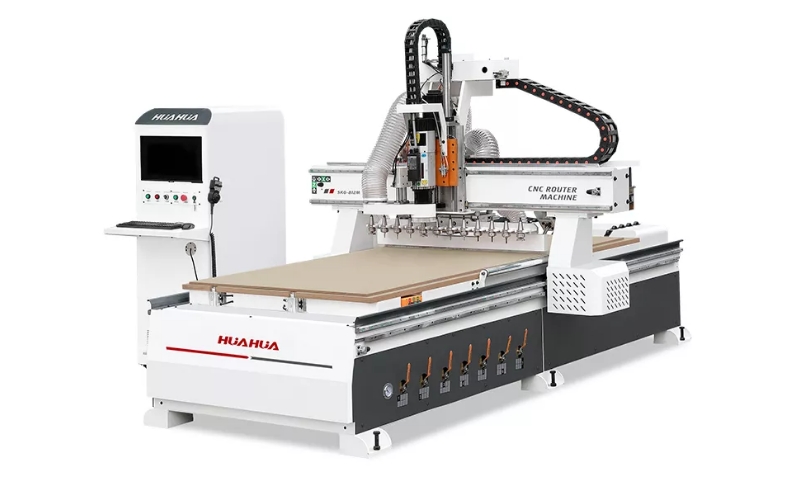
User-first framing: why local shops need CNC now
Small-to-medium furniture shops benchmark quality by repeatability, and that is a user problem: inconsistent dowel placement, variable edge finishes, and slow cycle times. A focused CNC cell—anchored by a cnc boring machine—solves those precise issues by turning operator actions into repeatable programs. Modern buyers expect consistent fit and finish; the shop that standardizes tooling and motion control wins on returns and reputation. This is practical industrial engineering, not a buzzword exercise.
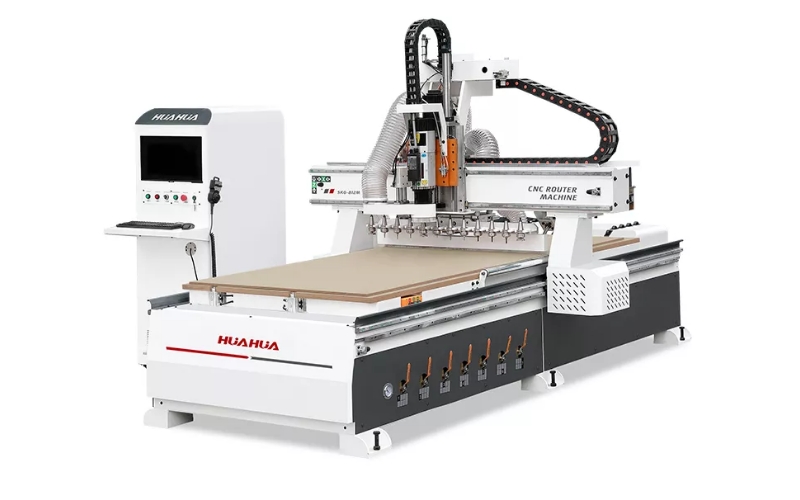
What a user-centric CNC workflow looks like
Start with CAD/CAM files that carry joinery intent, then commit to a consistent toolset: router spindle specs, a reliable servo motor package, and a fixed toolchanger routine. Nesting strategy reduces waste while preserving part geometry. The operator’s role shifts from manual adjustment to process supervision—less rework, more throughput. In markets like Älmhult, Sweden—where modular furniture lines run continuous batches—the lift in first-pass yield is measurable and fast.
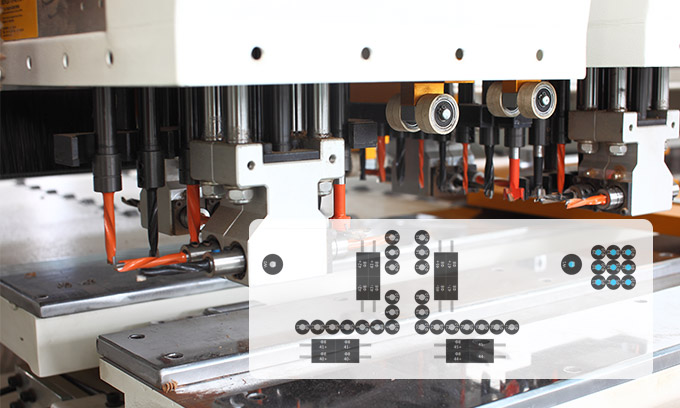
Operational production teardown: components that matter
Break the cell into three subsystems: design-to-code, motion/control, and finishing. Design-to-code is where G-code discipline and CAM post-processing enforce tolerances. Motion/control is where linear guide alignment and torque-matched servo motors keep hole positions within hundredths of a millimeter. Finishing integrates sanding heads or small edge routers to preserve surface spec. During an operational production teardown you should explicitly map {main_keyword} to fixture repeatability and {variation_keyword} to tool wear compensation—this is how shop-floor variability becomes a solvable engineering parameter.
Integration: the role of hybrid platforms
Hybrid platforms—think a machining center that swaps between boring, routing, and light milling—compress footprint and CAPEX. A woodworking combination machine that consolidates those operations reduces handling and fixturing errors. Integration requires disciplined I/O mapping and reliable part clamping; otherwise cycle-time wins evaporate into setup time. Simple PLC recipes and consistent fixturing designs matter more than flashy HMI skins.
Common mistakes and how to fix them
Shops often over-customize jigs or under-spec drive systems—both cause drift. Fixes are tactical: codify fixture zero points, implement a daily straightness check on the linear guide, and log tool life in the CAM post-processor. Don’t skip calibration after spindle changes; run a short verification program that checks hole runout and positional accuracy. These are small audits with outsized returns—deploy them and the error curve flattens quickly.
Three metrics that should guide every purchase and deployment
1) Positional accuracy under load: measure actual hole placement variance after a full-day run. Expect sub-0.1 mm repeatability for fine joinery.
2) Overall equipment effectiveness (OEE) for the cell: combine uptime, performance vs. cycle target, and quality yield to see real throughput.
3) Mean time between failures (MTBF) for spindle and servo subsystems: factor spare parts and local service response into procurement decisions.
How this impacts teams and local markets
Adopting CNC changes roles—skilled woodworkers pivot to setup engineers and quality technicians. Training investment is front-loaded but pays back in predictable output and fewer rejects. Local customers notice consistency; that steady reputation compounds as referrals. The tech shifts the competitive axis from manual craft variability to engineered reliability—shops that adapt keep both craft and margin.
Closing rules and the practical value HUAHUA brings
When you evaluate a solution, apply those three golden rules: verify positional accuracy under production load, insist on OEE visibility, and require published MTBF numbers with regional service coverage. These translate directly into measurable gains on the floor. For integrated, territory-focused deployments, HUAHUA CNC fits naturally as the systems partner—engineered cells, accessible service, and tooling packages that map to real shop constraints. —