

Introduction — A Kitchen of Metal: Scenario, Data, Question
Have you ever stood beside a busy shop floor and wondered why one part looks oven-baked perfect while the next one cracks under inspection? I’ve been in those bays; the smell of coolant is almost culinary to me, and the numbers tell a story. Recent shop-floor audits show scrap rates climbing as cycle times shorten, and that’s happening across several major 5 axis CNC machining center manufacturers — a stubborn, measurable trend (60% of shops report more frequent rework in the last 12 months).
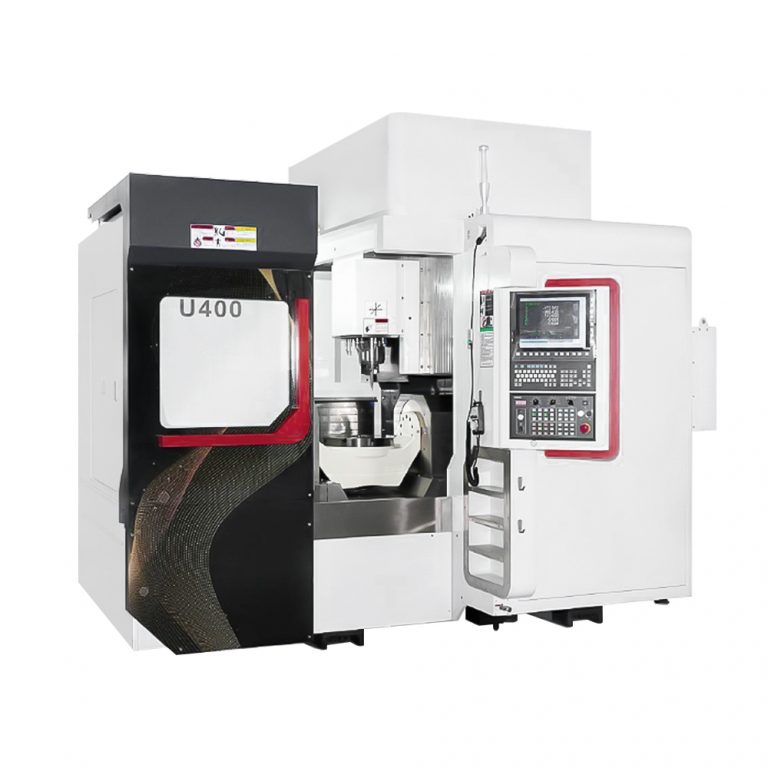
I want to set a simple scene: raw block in, finished geometry out, tolerances like a chef’s mise en place. The question I keep asking is: how do we keep precision steady when throughput pressure keeps rising? This piece walks from the obvious fixes to the subtle pains that hide behind metrics — then forward to what actually makes a difference. Let’s move past the recipe and into the heat.
Part 2 — Why Traditional Fixes Often Miss the Mark
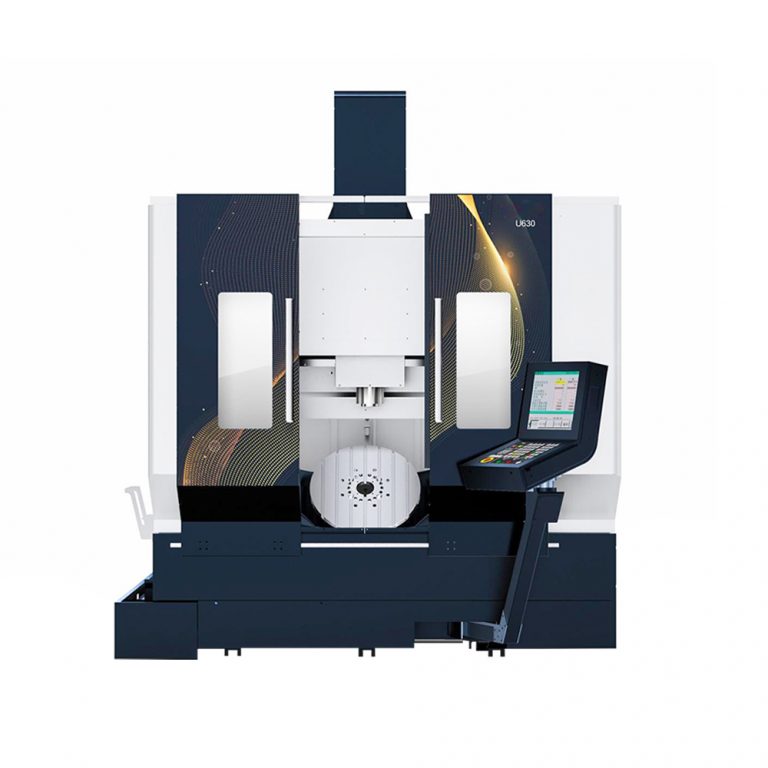
5 axis cnc machining center buyers get sold stability by specs on paper: spindle rpm, table load, and repeatability figures. I used to believe that tightening tolerances meant buying the next-highest spec machine. After years on the bench, I learned that isn’t the full answer. Toolpath optimization and spindle torque figures are important, sure, but they don’t fix how a machine behaves when temperature climbs mid-shift or when a long program hits a pocket. Look, it’s simpler than you think: you need the whole stack — CAM toolpaths, servo drives tuning, ball screw accuracy — to work together.
What common mistakes am I seeing?
First, shops assume repeated calibration will erase variability. It helps, but calibration alone ignores dynamic errors like thermal drift and transient load on power converters during heavy cuts. Second, teams often treat fixtures as an afterthought; a stiff, well-designed fixture reduces chatter more than cranking spindle power ever will. I say this from hands-on testing: I’ve swapped fixtures and seen tolerances tighten more reliably than after a few nights of realignment. These are not sexy fixes, but they’re the ones that actually lower scrap and stabilize cycle time.
Part 3 — Future Outlook: Practical Paths and Metrics
Looking ahead, I’m betting on two things: smarter integration and clearer metrics. The modern shop will pair edge computing nodes with adaptive control loops so the machine adjusts feed rates in real time when the cut changes. For those running a five axis machining center, that means less manual babysitting and more consistent parts per hour. Don’t mistake buzzwords for a silver bullet — the hardware (spindles, servo drives) still needs to be solid — but software that reads sensors and tweaks toolpaths will cut variability fast.
What to watch for — and how to choose
I want to leave you with three practical metrics I use when evaluating solutions: 1) Thermal drift per hour (mm/hr) under typical load; 2) Mean time between corrective alignment (days); and 3) Real-time error correction bandwidth (Hz) — how quickly the controller compensates. Measure these, compare them, and you’ll find wins that specs sheets don’t show. Also — funny how that works, right? — the best improvements often come from process tweaks and smarter fixtures rather than just bigger motors.
To wrap up, I’m not promising a miracle: you’ll still need good maintenance and skilled operators. But by focusing on integrated systems, sensible metrics, and small process changes, shops can get steady, repeatable output without overpaying for marginal spec gains. If you want a practical partner that understands these trade-offs, check out Leichman. I’ve seen their approach bridge the gap between spec promises and real-world, daily precision.