

Introduction — a small shop moment, some numbers, and a question
I remember watching a late shift where a single bad setup cost us an entire morning of production (we all have those days). CNC milling and turning centers were humming—spindles spinning, programs running—but output didn’t match the hours logged. Data from that week showed cycle times creeping by nearly 12% on average across mixed jobs. So I asked myself: how do we stop losing time to small, repeated inefficiencies and actually raise throughput without breaking the bank?
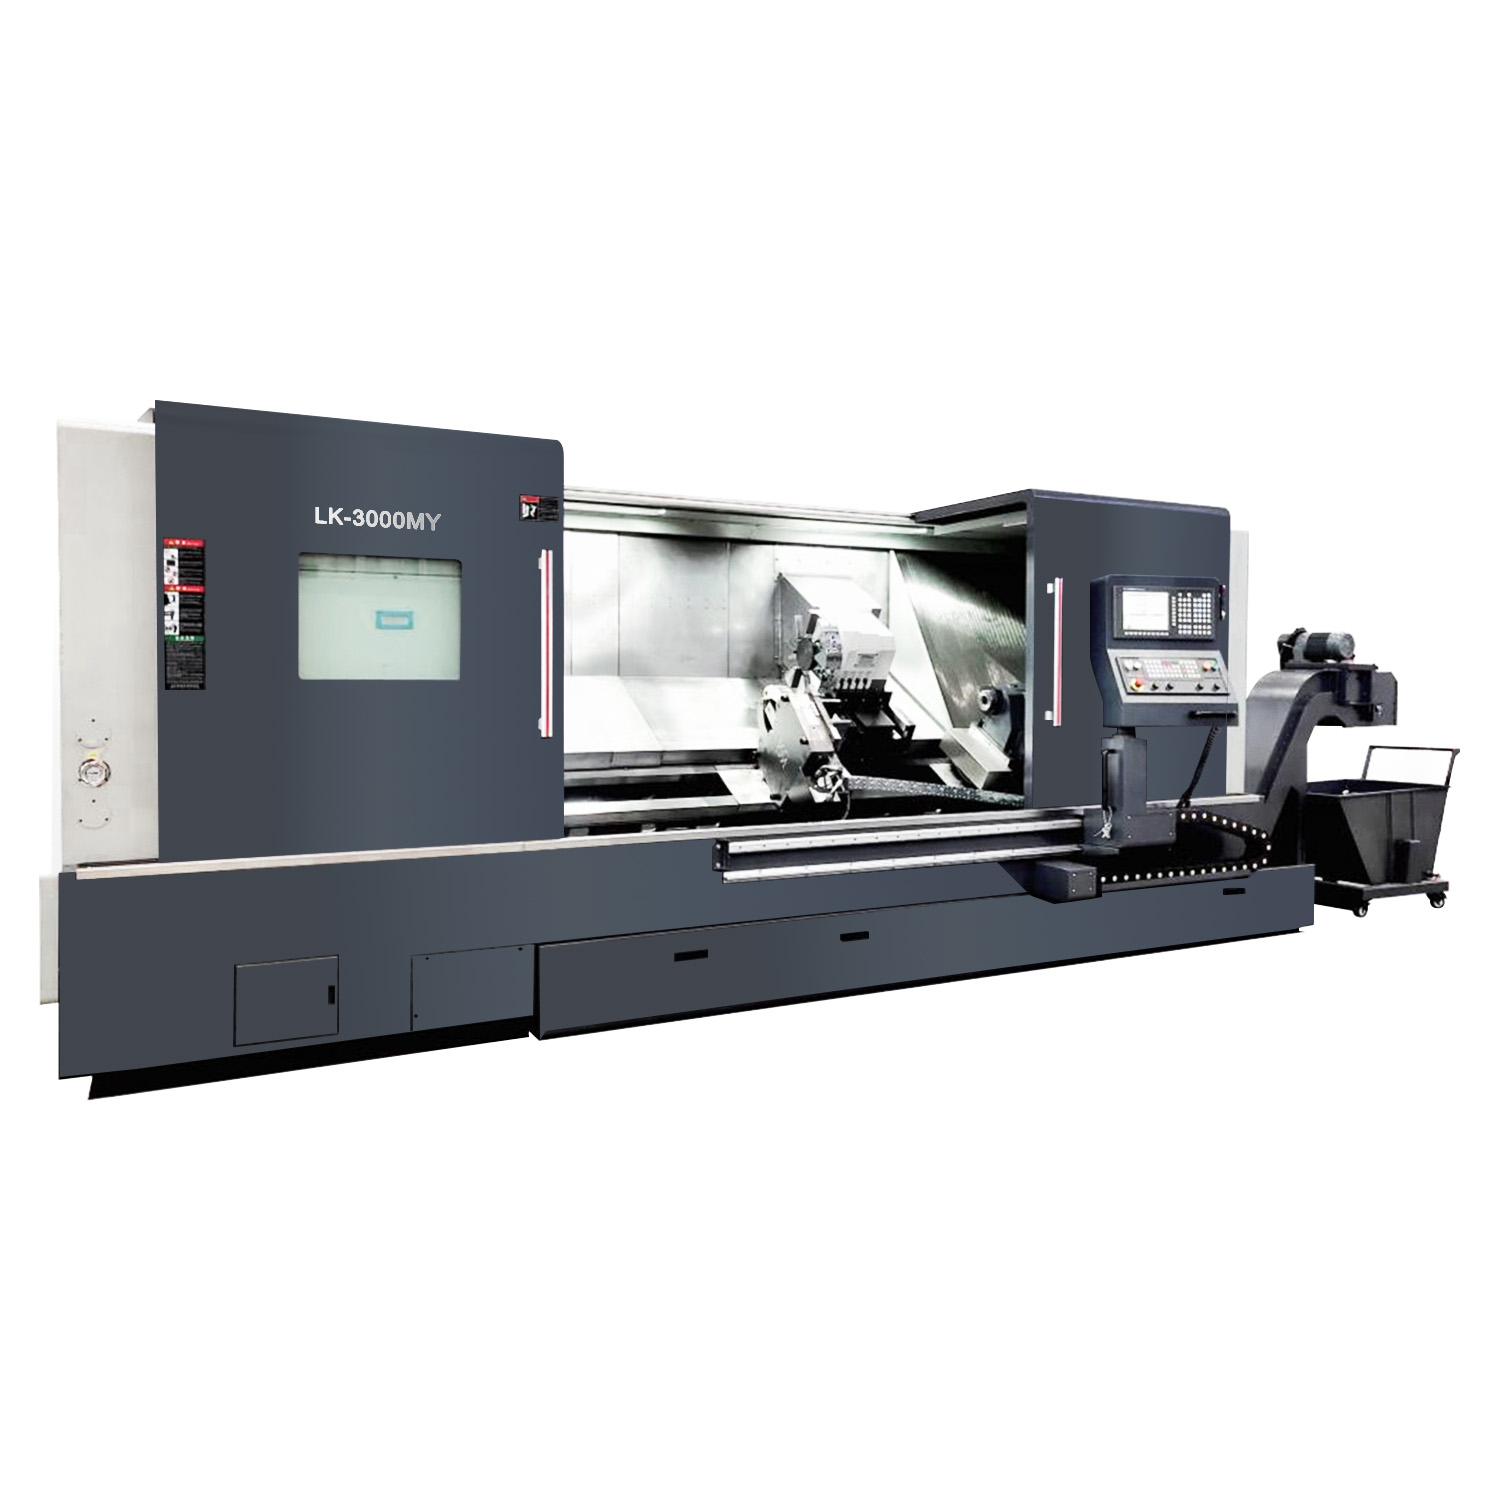
I want to be practical with you. Start small. Look at spindle idle time, tool change delays, and how often programs require manual intervention. These are the places where simple fixes deliver the largest gains. I’ll walk through what I’ve seen work (and what tends to fail), and then we’ll compare options so you can pick what fits your floor. Ready? Let’s dig in—there’s a solid path forward here.
Why traditional approaches fail: digging under the hood of a milling and turning machining center with y axis
milling and turning machining center with y axis often gets pitched as the single answer to mixed-process work. I’ve seen them perform wonders, but they also expose hidden weaknesses in legacy approaches. On paper, a Y-axis and servo turret promise fewer setups and higher part consolidation. In reality, issues like poor axis compensation, slow toolchanger sequences, and non-optimized feedrate tables turn potential gains into schedule risk. Look, it’s simpler than you think: the machine’s capability only helps if the process, fixturing, and CAM strategies match it.
What usually trips shops up?
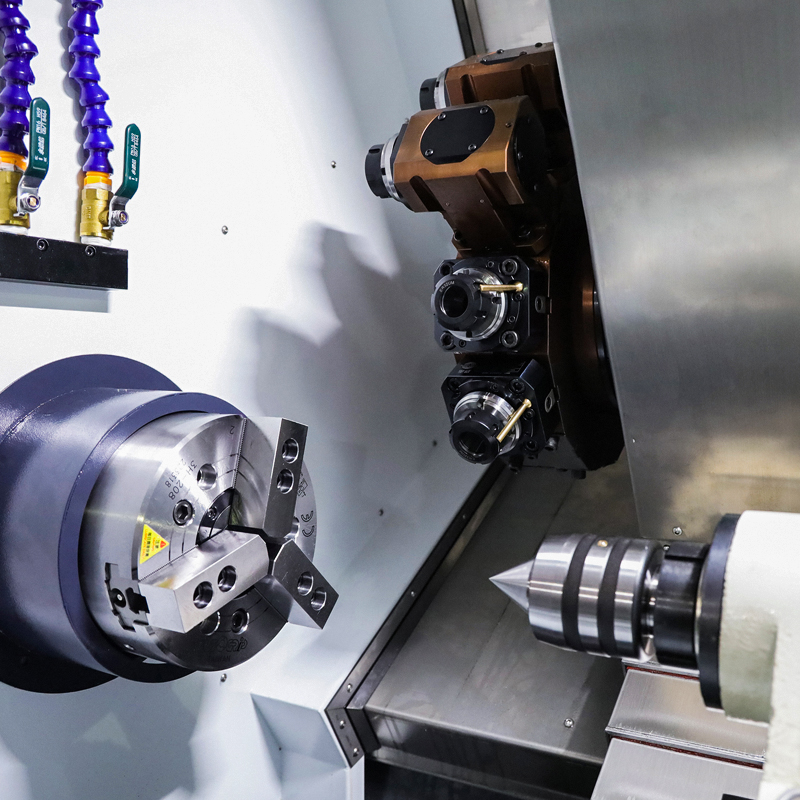
First, programs written without regard for spindle dynamics create chatter or require reduced RPMs. Second, fixturing that worked on a 3-axis mill suddenly reveals torque and clearance issues when the Y-axis shifts load vectors. Third, communication gaps between the CNC controller and plant MES mean tool life isn’t tracked—so we change tools too early or too late. These are not glamorous problems, but they are the ones that rob consistent throughput. I’m speaking from hands-on fixes: retune spindle maps, standardize tool-pocket assignments, and audit G-code for efficient peck cycles. Small, repeatable corrections add up fast — funny how that works, right?
New principles and practical choices for the next step
Looking forward, I recommend grounding decisions in three principles: match machine kinematics to the job mix, optimize the digital thread, and prioritize maintainability. When cnc milling and turning manufacturers discuss upgrades, they often focus on hardware—bigger motors, more axes. That helps, but the real lift comes from combining those upgrades with better CAM strategies and smarter tool libraries. We should consider sensor-driven adjustments (spindle load sensing, tool-life telemetry) and tighter integration with the CNC controller so adjustments can be automated instead of manual.
What’s Next: quick wins and a roadmap?
Start by piloting on one part family. Measure baseline cycle time, scrap, and setup hours. Then try targeted changes: refine toolpaths to reduce air moves, normalize torque settings so the Y-axis isn’t overcompensating, and introduce simple condition monitoring. Evaluate results after a set run — 50–100 parts — and decide whether to scale. For choosing solutions, I suggest three metrics: cycle time reduction (%), setup time saved (minutes per job), and mean time between failures (hours). Use those to compare vendors and software. I’ve seen these metrics turn vague promises into clear choices — and yes, they help you avoid shiny-but-irrelevant upgrades.
In closing, I’ll be frank: the best gains come from a mix of modest hardware alignment and disciplined process work. We don’t need to reinvent the floor. We need focused fixes, measurable tests, and a vendor who understands your part mix. If you want a starting point or a checklist, I’ll happily share what I use on the shop floor. For reference and support, check out Leichman — they’re a good conversation starter when you’re ready to compare options.